三年免费观看免费大全_三年成全免费观看完整版_三年大片在线观看免费观看爱奇艺_三年免费观看完整版免费高清_三年在线观看中文免费_三年影视三年大片高清影视大全免费_三年哔哩哔哩免费观看电视剧大全_三年大片观看免费国语版_三年成全免费观看大全电视剧三_三年中文在线看完整版百度

展開

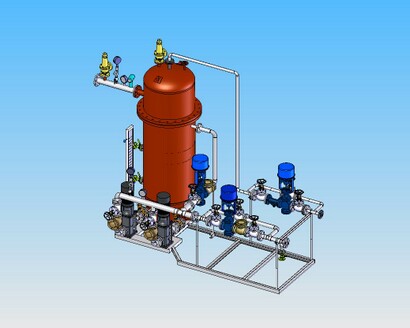
Exhaust steam suction recovery unit

Exhaust steam recovery device is an energy?saving product that supports environmental protection and energy conservation. It is used for exhaust steam recovery from boiler deaerators in thermal power plants across industries including thermal power, petrochemical, light industry, textile, food, papermaking, steel, and heating supply.

Download Exhaust steam suction recovery unit
Features

Structure

The exhaust steam suction recovery device consists of a suction jet pump and a recovery device body. The suction jet pump comprises an exhaust steam ejector, a mixing chamber, and a subsequent heat exchange system. The recovery device body is composed of a cavitation elimination device, a decontamination unit, a water collection vessel, a butterfly valve, a manual control valve, a high?temperature water transfer pump, and a control system.

Scope of Application

This device is suitable for recovering low?pressure exhaust steam from heating equipment in industrial facilities, high?temperature low?pressure exhaust steam from boiler continuous blowdown and deaerators, turbine exhaust steam, and condensate flash steam. Purified ambient water is used to aspirate this exhaust steam, and through sufficient heat exchange, high?temperature clean water is produced for industrial and domestic use. The unit can recover exhaust steam and low?temperature low?pressure steam or secondary flash steam within a pressure range of 0.02 MPa to 1.0 MPa, delivering hot water at temperatures from approximately 60 °C to 90 °C.

Control Scheme

Pump start?stop in the exhaust steam suction recovery device is primarily governed by liquid level signals, with centralized system control. The liquid level signal is a 4–20 mA two?wire output, transmitted to the control cabinet to regulate pump frequency operation and valve actuation. Temperature is monitored via platinum resistance sensors, with signals fed to the PLC to control the opening and position of the regulating valve on the power water line.

Key Features

1.Low?Pressure Suction Capability – A unique power?driven suction device based on the Venturi principle creates a relative “negative pressure zone” at the steam inlet, facilitating exhaust steam discharge without affecting upstream process conditions.

2.Low Noise and Vibration – A specially designed internal structure effectively mitigates water hammer during steam?water mixing, ensuring quiet and stable operation.

3.High?Efficiency Steam Recovery – Advanced suction technology enables near?complete recovery of process exhaust steam, significantly reducing thermal pollution and supporting energy conservation and clean production.

4.Cavitation Prevention – Dynamic two?phase flow technology combined with micro?subcooling eliminates cavitation when pumping high?temperature water, ensuring reliable delivery to designated points.

5.Automatic Unattended Operation – Intelligent control enables fully automated, maintenance?reduced operation with minimal manual intervention.


2.jpg

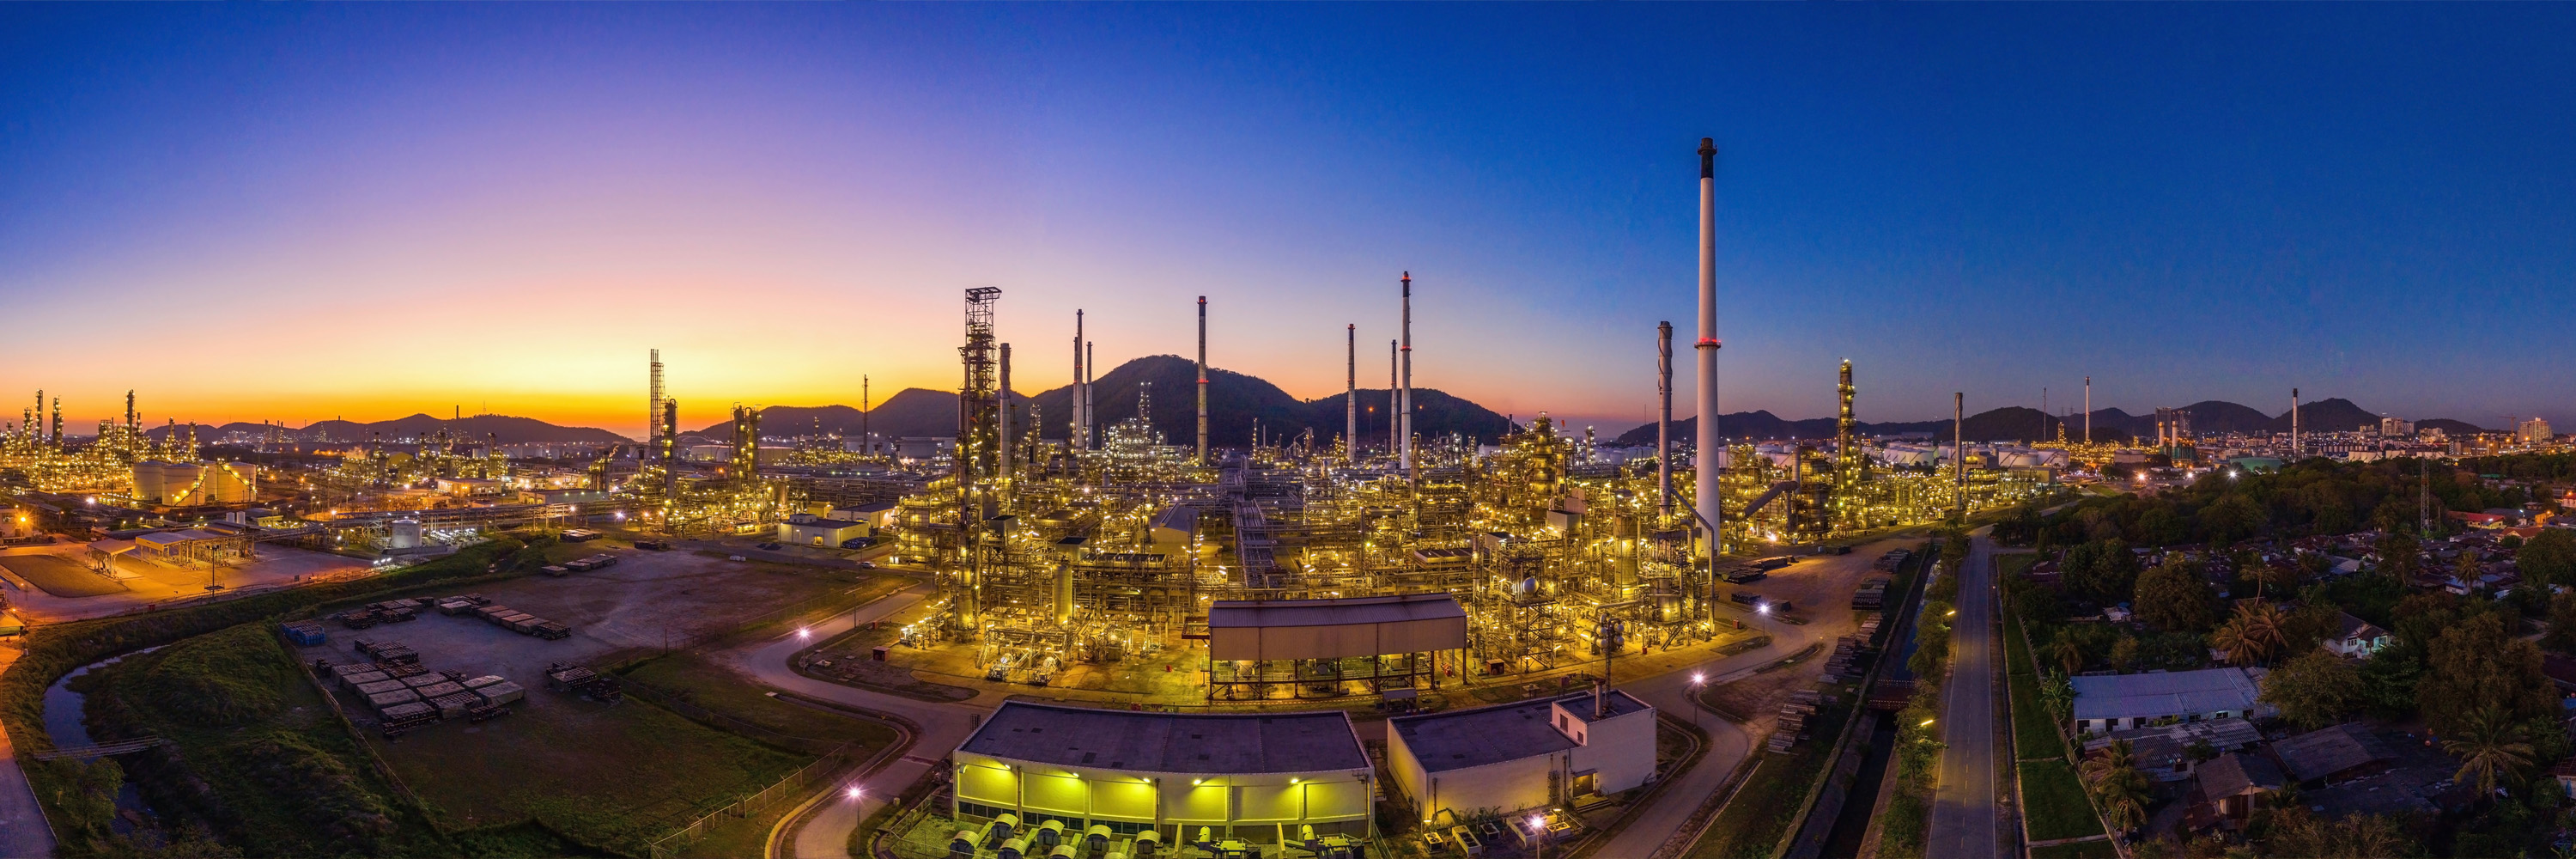
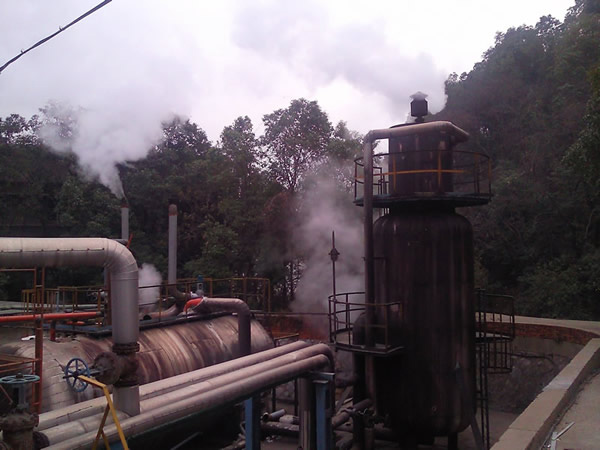
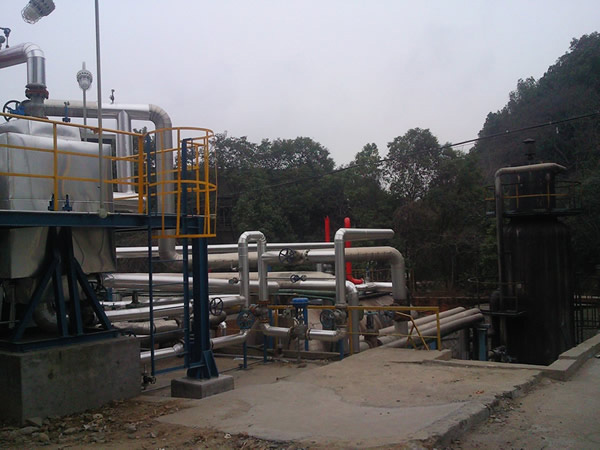
On-site comparison diagram of a petrochemical enterprise before and after the application of exhaust steam recovery device 

選型速查表
Information Request
* Please fill in your email address truthfully, and the product information will be sent to your mailbox